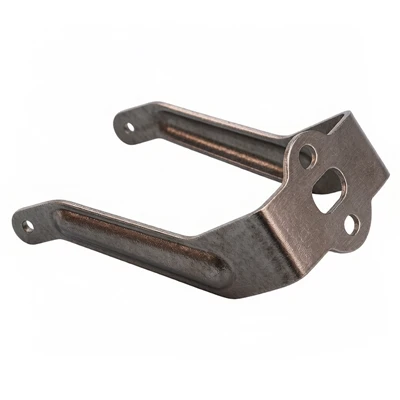
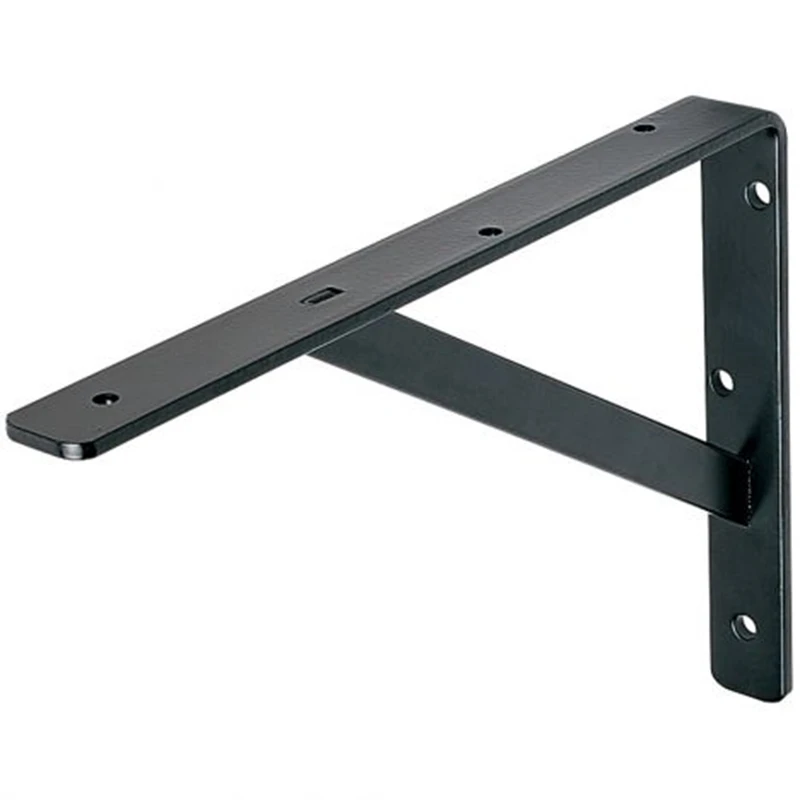


A deep drawn metal pressing component is a seamless shell formed by pulling flat sheet into a die under controlled draw ratios, producing cups, housings, covers and pockets without a welded seam. It is produced from DC03 deep-drawing cold-rolled steel, SUS304 or 6061 aluminum, with the grade selected for its draw ductility against the required depth. Stock thickness runs 0.5-4.0 mm across a 0.3-5.0 mm range, and the part is formed to keep the draw radius at least equal to sheet thickness so corners draw without cracking or splitting. Three-dimensional outer dimensions are held to +/-0.15 mm while inner cavity fit is tightened to +/-0.1 mm for precision assembly, and post-processing options include brushing, anodizing, powder coating or electroplating for the required appearance and corrosion level. The process covers irregular shells, brackets and cavities that would otherwise need multiple welded pieces, and tooling is built directly from the customer's 3D drawing or a physical sample. The process covers irregular shells, brackets and cavities that would otherwise need several welded pieces, and a physical sample can be reverse-modeled into a forming die when no CAD data is available.
The key purchase risk in deep drawing is split walls or uneven thinning when depth outruns the material's ductility. Because we select draw-grade strip per part and confirm geometry on a sample from the customer's 3D data, the draw radius, blank holder and deep-draw sequence are tuned to the actual shell depth - turning a part that could crack on the first hit into a repeatable formed component with stable wall thickness.

Specifications
|
Parameter |
Specification |
|
Material |
DC03 deep-drawing steel / SUS304 / 6061 aluminum |
|
Thickness |
0.5-4.0 mm (0.3-5.0 mm) |
|
Draw radius |
R >= sheet thickness |
|
Outer dimension tolerance |
+/-0.15 mm |
|
Inner cavity tolerance |
+/-0.1 mm |
|
Post-processing |
Brushing / anodizing / powder coating / plating |
|
Forming goal |
No cracks at deep draw, no fracture at bends |
Applications
Seamless electrical and appliance housings: one-piece drawn shells eliminate welded seams, which is why they are chosen where a clean, leak-resistant cover matters.
Deep pockets and cups for automotive and industrial use: controlled wall thinning keeps strength at the bottom radius without splitting the side wall.
Custom-shaped covers and brackets from 3D data: the +/-0.1 mm cavity fit lets the formed shell locate mating components accurately.
Customization
Material and strip selection by draw depth, full thickness range 0.3-5.0 mm, draw radius and depth tuning, outer and inner tolerance tightening for precision assembly, and surface finish (brushed, anodized, powder coated or plated), all tooled from customer 3D drawings or samples.
Packaging & Transportation
Formed shells are protected per product specification to preserve draw surfaces and plated finishes, with dedicated pre-dispatch inspection; third-party inspection is accepted. EXW, FOB or DDP terms.
FAQ
Q: Can you manufacture based on our technical drawings or prototypes?
A: Yes, we manufacture based on customer technical drawings or prototypes.
Q: How long does it take for custom sample development?
A: It depends on complexity: simple parts take 3-5 days, complex parts 5-10 days.
Q: Do you accept third-party inspections?
A: Yes, we accept third-party inspections.
Hot Tags: deep drawn metal pressing component, China deep drawn metal pressing component manufacturers, suppliers, factory, high precision stamping parts, sheet metal stamped parts, stamped metal clips, stamped metal retainers, stamped metal rings, stamped sheet metal components