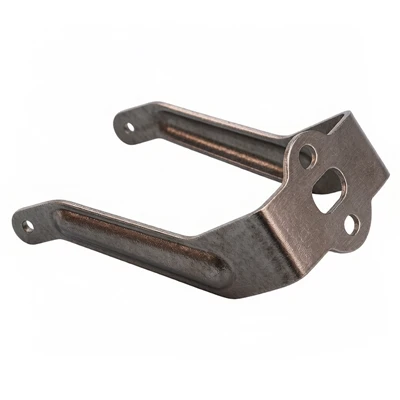


A progressive die pressed angle bracket gives equipment frames a rigid, one-piece mounting point where a welded angle or a loose clevis would otherwise be used. Purchasers look for a bracket that stands up to lateral force and vibration, aligns neatly with rack fixing points, and avoids the weak seam that appears where two pieces are welded together. Formed as a single bent part with integral strengthening ribs, the bracket carries load through its own body rather than through a weld bead, which keeps the connection stiff and consistent. Ductile steel suits the complex bends, with stainless or lighter alloy options for corrosion or weight needs, and a coated finish protects the frame in exposed or wash-down settings. Developed to a specific equipment-frame drawing, the part is engineered as a load-path support that holds racks, enclosures and machinery frames square and steady under ongoing vibration and cyclic load.
Because this bracket replaces welded joints, the hidden buyer worry is inconsistency: a one-piece stamping must prove its strength across every piece. Progressive-die forming keeps the rib layout and bend-root geometry identical shot to shot, which removes the weld-weak-point failure mode and holds the ≥100 kg lateral rating batch after batch. The no-weld process also lets rib pattern and frame geometry be re-drawn to fit a specific equipment rack, so the bracket is engineered to the load path rather than adapted to a generic angle. Shot-to-shot identity of the rib and bend root also removes the strength scatter that makes welded brackets fail at different points across a batch.

Specifications
|
Parameter |
Specification |
|
Material |
SPCC DC03 deep-drawing steel; SUS304 / aluminum optional |
|
Thickness |
1.5 / 2.0 / 2.5 / 3.0 mm; 1.2-4.5 mm custom |
|
Structure |
One-piece bend with integral stamping ribs, no weld |
|
Hole pitch cumulative tolerance |
≤0.12 mm |
|
Lateral push resistance |
≥100 kg, no bend-root cracking |
|
Coating |
Powder coat 70-100 μm |
|
Salt spray |
200 h neutral |
Applications
Vibration-prone machine frames: the weld-free one-piece body removes weld-seam cracking under continuous vibration and cyclic load.
Equipment rack and enclosure mounting: multi-group punched holes with ≤0.12 mm cumulative pitch align neatly to standard rack fixing points.
Corrosion-exposed installations: the 70-100 μm powder coat and 200 h salt-spray rating suit outdoor or wash-down environments.
Customization
Thickness 1.2-4.5 mm, rib layout and frame structure, hole count and spacing, overall length / width / height, bend angles and mounting features; produced to customer drawings and samples; OEM / ODM.
Packaging & Transportation
Brackets are stacked with separator sheets to protect the powder coat, cartoned and palletized for frame orders; a dedicated inspector checks each lot, with 100% inspection depending on the product. Trade terms: EXW, FOB or DDP.
FAQ
Q: Can the bracket be designed to our rack drawing?
A: Yes. Overall dimensions, bend angles, rib layout and mounting structure are all developed from your equipment drawing or sample.
Q: Do you accept third-party inspection?
A: Yes. A dedicated inspector checks each batch and we accept third-party inspection; 100% pre-pack inspection depends on the product.
Q: How are damaged brackets handled on arrival?
A: Handled case by case: small quantities are replaced directly; larger quantities are investigated to identify the cause and then replaced.
Hot Tags: progressive die pressed angle bracket, China progressive die pressed angle bracket manufacturers, suppliers, factory, aluminium stamping parts, metal stamping housings, metal stamping terminals, precision stamped components, stamped metal rings, stamped metal terminals