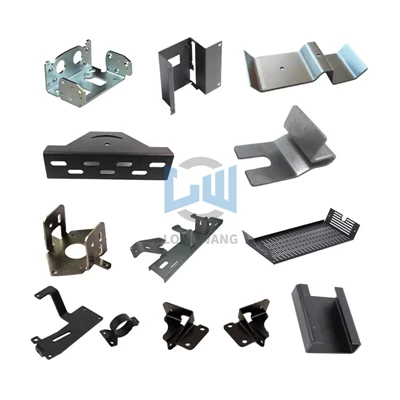


CNC press brake formed workpieces are pure-bent sheet metal parts whose value lives entirely in the accuracy of each bend. Starting from SPCC, DC03 deep-drawing steel, SUS304, or 5052 aluminum, material spans 0.6-5.0 mm so the same line covers thin-sheet micro-bends and heavy right-angle bends on thick plate. The minimum inside bend radius is held at or above material thickness to avoid cracking under tension on the outer bend. 90-degree bend angle tolerance is controlled to ±0.3 degrees, the flat blank (unfolded) dimension is held to ±0.15 mm, and overall length and width to ±0.2 mm, with precision parts tightened to ±0.08 mm. Common geometries include L, U, Z, and C profiles as well as multi-stage continuous bends, arc bends, and combined forms. After bending, secondary operations such as tapping, flanging, embossing, and chamfering can be applied, followed by uniform deburring and plating or powder coating. High-ductility grades are selected for complex multi-stage forms to reduce springback and edge cracking.
For bent parts, the buyer's real risk is batch-to-batch angle and dimension drift, not whether a single prototype bends well. CNC press brake control keeps bend angle and blank dimensions repeatable run after run, so repeated orders drop into the same assembly without refixturing or rechecking every profile. Choosing the right ductile grade, such as DC03 deep-drawing steel for Z-profile parts, also removes the cracking failures that thinner or less ductile sheet tends to produce at bend roots, which is what matters when a profile has to bend cleanly in production volumes rather than in a one-off sample. Consistent bend sequencing across the run is what keeps a whole order of channels fitting the same mating parts.

Specifications
|
Parameter |
Specification |
|
Material |
SPCC, DC03 deep-drawing steel, SUS304, 5052 aluminum |
|
Thickness |
0.6-5.0 mm |
|
Min. Inside Bend Radius |
≥ material thickness |
|
90° Bend Angle Tolerance |
±0.3° |
|
Blank Dimension Tolerance |
±0.15 mm; precision ±0.08 mm |
|
Overall Length/Width |
±0.2 mm |
|
Post-Process |
Tapping, flanging, embossing, chamfering, deburring, plating/powder coating |
Applications
Structural profiles in enclosures: L/U/Z/C bent channels act as rigid frames that bolt directly to mating panels.
Mounting rails and brackets: controlled bend angles let the profile locate components without shimming during assembly.
Multi-section and arc-bent housings: ductile-material bending forms complex profiles without root cracking, replacing welded assemblies.
Customization
Produced from customer drawings. Multi-stage, arc, and combined bend geometries are supported; thread sizes, flange heights, emboss positions, and local protective coatings are all customizable.
Packaging & Transportation
Workpieces are deburred and then packed to specification to protect edges and plated surfaces from scratch and collision. Pre-pack inspection is performed according to product, and third-party inspection is accepted. Trade terms EXW, FOB, and DDP are available.
FAQ
Q: Can you provide a prototype/sample before mass production?
A: Yes, a sample can be provided before bulk production.
Q: How long does it take for custom sample development?
A: It depends on complexity: simple samples take 3-5 days, complex samples 5-10 days.
Q: Do you accept third-party inspections?
A: Yes, we accept third-party inspection.
Hot Tags: cnc press brake formed workpiece, China cnc press brake formed workpiece manufacturers, suppliers, factory, bent sheet metal components, cnc sheet metal components, sheet metal electrical components, sheet metal fabrication components, sheet metal supports, sheet metal welded assemblies